
NXT has built strong expertise across multiple industry sectors, in part through collaborations with specialized partners. As a certified integrator for leading innovators like 3M, Haffmans, and Sudmo, NXT works with proven, pre-engineered technologies. Some of this equipment is already manufactured and available for testing or rental, offering clients a faster path to evaluate and implement high-performance solutions.
NXT
Showing 1–16 of 17 results
-
Beer Chamber Pasteurizer – For Pro Breweries
The ideal solution for craft breweries looking to extend their product shelf life
Benefits
- Compact and cost-efficient: Requires minimal floor space and investment compared to tunnel pasteurizers.
- Energy-saving and easy to operate: Simple batch process with low power consumption and quick setup.
- Improves product safety and shelf life: Ensures consistent pasteurization for stable, contamination-free beverages.
-
Bulk bag unloader
Bulk Bag Unloader – Efficient, Dust-Free Handling of Bulk Ingredients
Benefits
- Dust-Free Operation – Integrated dust containment keeps your workspace clean and compliant.
- Efficient Material Flow – Designed to prevent clogging and ensure consistent discharge.
- Versatile Compatibility – Handles a wide range of bulk materials, from malt to powders and granules.
- Robust & Hygienic Design – Built with durable, food-grade materials for long-lasting performance.
- Customizable Options – Available with hoists, loss-in-weight systems, and flow aids for tailored efficiency.
Reduce manual labor, increase efficiency, and maintain a clean production environment with the Bulk Bag Unloader—the smart solution for handling bulk ingredients with ease.
-
Clean-in-place systems
Ensure peak performance and product quality with NXT Process’ Clean-in-Place (CIP) Systems—a fully automated solution designed to clean your brewing and processing equipment with minimal downtime. Say goodbye to manual cleaning inefficiencies and hello to a streamlined, consistent sanitation process that saves time, water, and chemicals.
Benefits
- Automated & Consistent Cleaning – Reduce labor costs and human error with a fully programmable system.
- Water & Chemical Savings – Optimized cleaning cycles minimize resource consumption without compromising hygiene.
- Compact, Modular Design – Fits seamlessly into any brewery or production facility, large or small.
- Regulatory Compliance – Ensures your equipment meets the highest industry sanitation standards.
- Customizable for Your Needs – Tailored solutions for breweries, food processing, and industrial applications.
-
CO2 recovery systems
Reduce your brewery’s carbon footprint and save on operational costs with NXT’ CO₂ Recovery Systems. Designed for professional breweries, this system captures, purifies, and reuses the CO₂ generated during fermentation, cutting your reliance on costly external gas supplies.
Benefits
- Cost Savings – Slash your CO₂ expenses by recycling what your brewery naturally produces.
- Sustainability – Reduce greenhouse gas emissions and improve your environmental impact.
- Efficiency – A fully automated system that seamlessly integrates into your existing process.
- Purity Guaranteed – Advanced filtration ensures brewery-grade CO₂ for optimal beer quality.
- Compact Design – Engineered to fit within limited brewery spaces without compromising performance.
Whether you’re a craft brewery or a large-scale operation, our CO₂ Recovery System ensures a smarter, greener, and more cost-effective brewing process. Invest in sustainability without sacrificing efficiency.
-
Deoxygenator
Our modular in-line membrane deaeration system removes almost all oxygen from water in just a few minutes.
Benefits
- In-line deaeration for liquid between 6 ° C and 20 °
- CIP able
- Allows you to remove almost 100% of the O2
- Available for purchase and rental
- Centrifugal pump addition option
- More membranes can be added to achieve higher flow
The NXT DEOX deoxygenation system using Liqui-CelTM membrane contactors can be installed directly on the production line. For process water flowing at 60 hl / h (~ 26 gpm), two Liqui-Cel 8×20 membrane contactors arranged in series are required to remove almost 100% of the dissolved oxygen.
-
Drum unloader
With two different tracking plates to accommodate various barrel diameters, a state-of-the-art interface and an electric drum pump, the QDU provides sanitary and fast unloading.
Benefits
- Cleaning in place (CIP)
- Stainless Steel Structure
- Quiet Operation
- Washdown Type Motor
- Continuous Flow
- FDA & EHEDG Certified
-
Heating and cooling systems
Ensure precise thermal regulation for any liquid process with a custom Heating & Cooling System from NXT Process. With years of experience designing systems for breweries, food production, and industrial liquid processing, we provide optimal thermal management—enhancing energy efficiency while preserving product quality and consistency.
Benefits
- Accurate Temperature Control – Delivers precise heating and cooling to maintain optimal process conditions.
- Energy-Efficient Design – Reduces energy consumption while maximizing thermal performance.
- Seamless Integration – Compatible with existing process systems for hassle-free implementation.
- Fast & Consistent Performance – Ensures uniform temperature distribution for improved product quality.
- Customizable Solutions – Tailored to your specific process requirements and capacity needs.
-
Hop incorporator
Enhance your brewing process with the Hop Incorporator, designed for precise and efficient hop additions. This system ensures optimal extraction of hop aroma and flavor while reducing waste and improving consistency. Perfect for dry hopping, late-stage additions, and other flavor infusion applications, it seamlessly integrates into your brewing operation.
Benefits
- Cold hopping minimizes oxygen supply
- Suitable for any addition during fermentation: Hops, coffee, fruits, spices, etc.
- Reliable CIP
- Safe recirculation flow control
- Ensures an efficient and consistent beer profile
- Available for purchase and rental
- Clamp container
-
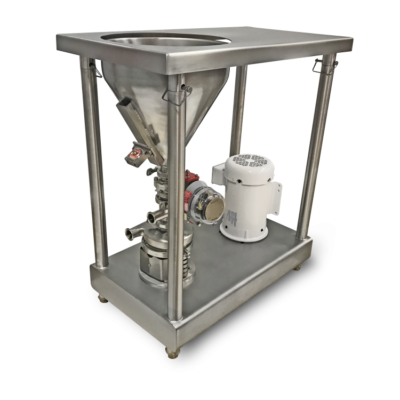
Inline powder mixing systems
Increase efficiency, improve product consistency, and streamline your operations with the Inline Powder Induction System—the smart choice for precision mixing.
Benefits
- High-Efficiency Mixing – Achieves uniform powder dispersion directly into liquid streams.
- Clump-Free Performance – Prevents clogging and ensures smooth, homogenous blending.
- Dust-Free Operation – Minimizes airborne particles for a cleaner, safer work environment.
- Reduced Waste & Energy Use – Maximizes ingredient utilization while lowering processing costs.
- Customizable for Your Process – Available in multiple configurations to meet your production needs.
-
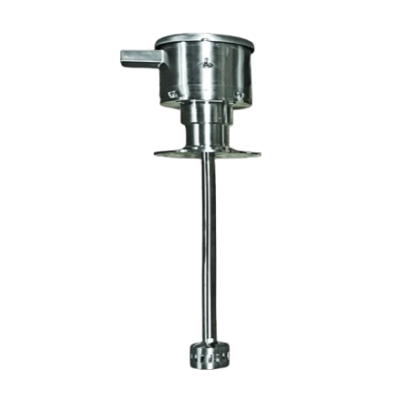
JET-shear in-tank mixer
Achieve superior mixing, emulsification, and dispersion with the Jet Shear, an advanced inline shear mixer designed for high-efficiency liquid processing. Ideal for breweries, food production, and industrial applications, this system ensures uniform blending, reduces processing time, and eliminates clumps for a smooth, high-quality final product.
Benefits
- High-Shear Mixing – Ensures rapid, uniform dispersion of powders, liquids, and emulsifiers.
- Clump-Free Consistency – Eliminates lumps and improves ingredient integration.
- Inline Efficiency – Continuous processing for faster production and reduced batch times.
- Sanitary & Easy to Clean – Hygienic design meets food and beverage industry standards.
- Customizable for Your Process – Available in various sizes and configurations to fit your production needs.
-
Mixing systems
Whether you’re blending ingredients, homogenizing liquids, or dissolving solids, NXT Process mixing systems delivers unmatched efficiency, product consistency, and resource savings.
Benefits
- Consistent, High-Quality Blends – Achieve uniform product quality with precision-engineered mixing technology.
- Energy & Resource Efficiency – Reduce waste, lower operational costs, and optimize ingredient usage.
- Customizable for Any Application – Tailored solutions for breweries, food production, and industrial processes.
- Hygienic & Easy to Clean – Designed for seamless integration with Clean-in-Place (CIP) systems.
- Compact, Space-Saving Design – Fits efficiently into your facility without compromising performance.
-
Mobile pump
Just the best pump you can carry everywhere
Benefits
- Motor in steel, washdown or stainless steel
- Diameter for inlet and outlet port: 1/2 “, 1”, 1.5 “, 2”
- Different seal depending on the product to be pumped
- Motor power supply: 230, 460 V or 575 V
- Motor power (HP): 1/3 to 10 hp
-
NXT static mixer
Efficient mixing. Zero moving parts. Maximum ROI.
Benefits
- No moving parts – zero maintenance, zero downtime
- Compact and efficient – reduces footprint and eliminates the need for mixing tanks
- Versatile – ideal for food & beverage, hydrometallurgy, chemical, and industrial applications
- Custom engineered – optimized for your flow rate, viscosity, and mixing requirements
- Sustainable by design – cuts energy use and improves product consistency
-
Pentair bmf beer filtration membrane
One unit, perfect filtration. This membrane filtration system provides reliable, flexible, and long-lasting filtration, enhancing your brewing process with superior efficiency and quality.
Main Benefits
- Continuous filtration: And with automation, filtration can be uninterrupted.
- Less waste: Reusable membranes eliminate the need to dispose of filter media waste, reducing solid waste by up to 50%.
- Cost savings: Since no filter media waste is produced, this can mean lower disposal costs for your brewery.
- Quality: Iron capture is avoided when a diatomaceous earth filter aid is not used, which reduces the aging process and improves the beer’s taste stability.
-
Pigging systems
A superior way to get all your products
Benefits
- Reduction of product losses (recovery rate over 99.5%)
- Suitable for pigging all types of products conveyed through piping (viscous, loaded, solidifying, etc.)
- Greater flexibility in line use by limiting the risk of cross-contamination
- Elimination of dilution caused by water pushing without a pig
- Reduction in the volume of effluent to be treated
- Lower consumption of cleaning agents and fewer cleaning cycles
- Reduced operating costs and return on investment within the first year of use
- Custom-designed system that adapts to all types of needs and constraints